Industrial induction heating is a controlled, non-contact method of heating electrically conductive materials by generating heat directly inside the workpiece. Unlike furnaces or flame heating, the process does not rely on heating the surrounding air first. Instead, an alternating electromagnetic field induces electrical currents in the metal, allowing manufacturers to heat a specific area quickly and repeatedly.
However, understanding the basic principle is only the beginning. In an industrial process, heating performance depends heavily on operating frequency, output power, workpiece material, heating depth, coil geometry and coupling distance.
For manufacturers selecting an industrial induction heating system, these parameters determine whether the equipment can achieve the required temperature, heating depth, cycle time and production consistency.
This guide explains how industrial induction heating works and, more importantly, how the main process variables affect equipment selection.

How Does an Industrial Induction Heating System Generate Heat?
A typical induction heating process can be understood in four stages:
Power supply → induction coil → electromagnetic field → heat inside the workpiece
The induction heating power supply converts incoming electrical power into alternating current at the required operating frequency. This current flows through an induction coil, usually made from copper tubing.
When alternating current passes through the coil, it creates a rapidly changing electromagnetic field around it. A conductive metal workpiece placed within or near this field develops circulating electrical currents known as eddy currents.
Because the metal has electrical resistance, these currents generate heat inside the workpiece. This is why induction heating can heat metal without direct physical contact between the heating source and the part.
For ferromagnetic materials such as many carbon steels, magnetic effects can also contribute to heating below the material's Curie temperature. As the temperature and magnetic properties change, eddy-current heating becomes the dominant mechanism.
The actual result therefore depends not only on the induction heater itself, but also on the material and geometry of the component being processed.
What Components Make Up an Industrial Induction Heating System?
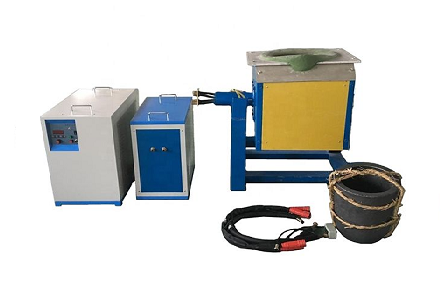
Although system configurations vary by application, a typical industrial induction heating installation includes:
· Induction heating power supply
· Inverter and control system
· Matching circuit or transformer where required
· Copper induction coil
· Cooling system
· Workpiece positioning or handling equipment
· Temperature or process monitoring
· Optional PLC, CNC, feeding or automation system
For continuous or higher-power industrial operation, cooling is particularly important. Hitfar's water-cooled induction heating machines use water cooling for the induction system and coil to support stable operation in applications such as brazing, hardening, annealing and other metal heating processes.
The correct system should therefore be selected as a complete heating process rather than simply by comparing equipment power ratings.
Why Is Induction Heating Frequency So Important?
Operating frequency is one of the most important parameters in an induction heating system because it strongly influences where the heat is concentrated inside the workpiece.
As a general engineering rule:
Higher frequency → more concentrated surface heating
Lower frequency → deeper heating into the workpiece
This relationship is connected to the skin effect. Alternating current tends to concentrate near the surface of a conductor, and this effect becomes stronger as frequency increases.
That means a high-frequency system may be suitable when a manufacturer needs rapid localized or surface heating, while a lower-frequency system may be more appropriate when heat needs to penetrate further into a larger cross-section.
Frequency should therefore never be selected only according to the highest available number.
It must match the:
· Workpiece diameter or thickness
· Material
· Required heating depth
· Heating temperature
· Production cycle
· Application process
Medium Frequency vs High Frequency vs Ultra-High Frequency
Hitfar provides induction heating equipment across different frequency ranges for different industrial heating requirements.
Frequency Type | Typical Heating Characteristic | Suitable Process Direction |
Medium Frequency | Deeper heat penetration | Forging, larger workpieces, through heating, melting |
High Frequency | Faster and more localized heating | Brazing, hardening, annealing, smaller components |
Ultra-High Frequency | Very concentrated surface/local heating | Precision brazing, small parts, fine hardening zones |
Hitfar's current medium-frequency equipment includes systems operating in the 1–20 kHz range, while high-frequency equipment includes systems around 30–150 kHz. Certain ultra-high-frequency models operate at 200 kHz and above.
These ranges should not be treated as universal selection rules. The ideal frequency still depends on the actual workpiece and heating target.
How Does Frequency Affect Heating Depth?
One of the most common mistakes when specifying an induction heating machine is focusing on heating speed without defining the required heating depth.
Consider two very different applications.
Surface Hardening
A shaft or gear may only require a hardened surface layer while retaining a tougher core.
In this situation, the process often requires relatively concentrated heating before quenching. A high-frequency induction heateror another appropriate frequency range may provide the localized energy distribution required for the process.
For production lines requiring controlled heating and subsequent quenching, a dedicated induction heating quenching machine can also integrate the heating process with part handling and quenching.
Bar or Billet Heating Before Forging
A steel billet that will be forged normally requires heat to penetrate much further into the cross-section.
Surface-only heating would create an unacceptable temperature difference between the outside and center of the material.
For this reason, medium-frequency equipment is commonly considered for larger workpieces and through-heating applications. Hitfar's induction heating forging furnace is designed around medium-frequency induction heating for forging applications.
The correct frequency is therefore determined by where the heat needs to go, not simply by how quickly a machine can heat the surface.
How Does Workpiece Material Affect Induction Heating?
Different metals respond differently to the same electromagnetic field.
Important material properties include:
· Electrical resistivity
· Magnetic permeability
· Thermal conductivity
· Specific heat
· Density
· Temperature-dependent material characteristics
Carbon Steel
Carbon steel generally responds well to induction heating and is widely processed using induction systems for hardening, forging, brazing and other heat-treatment operations.
Stainless Steel
Stainless steel can also be heated by induction, but different grades have different magnetic and electrical characteristics. The required power and cycle therefore need to be evaluated according to the exact alloy and component dimensions.
Copper and Aluminum
Copper and aluminum have high electrical and thermal conductivity. They can be heated using induction, but the system design may require different frequency, power and coil considerations compared with carbon steel.
When requesting an induction heating solution, buyers should therefore provide the exact material grade whenever possible, rather than simply stating "metal."
How Do You Select the Required Induction Heating Power?
Frequency determines the heating characteristics, while power strongly affects how much energy can be delivered within the required cycle time.
The power requirement depends on several factors:
· Workpiece material
· Workpiece mass
· Starting temperature
· Target temperature
· Required heating time
· Heating length or area
· Production rate
· Coil efficiency
· Heat loss during processing
· Continuous or intermittent operation
For example, heating one small steel component to brazing temperature every 20 seconds has very different power requirements from heating a continuous production stream of large steel billets before forging.
This is why selecting a machine only according to "15 kW vs 30 kW vs 60 kW" can produce poor results.
Before recommending equipment, the heating requirement should first be translated into:
material + dimensions + target temperature + heating time + production quantity
These five pieces of information provide a much better basis for initial equipment selection.
Why Is Induction Coil Design Critical?
The induction coil is not simply an accessory connected to the machine.
It is part of the electromagnetic heating system and directly affects:
· Heating position
· Heating uniformity
· Coupling efficiency
· Heating speed
· Energy concentration
· Repeatability
A coil should be designed according to the geometry of the workpiece and the area that must be heated.
Common configurations include:
· Single-turn coils
· Multi-turn helical coils
· Internal coils
· Flat or pancake coils
· Hairpin coils
· Contoured coils
· Custom scanning coils
A poorly matched coil may create uneven heating even when the power supply has sufficient capacity.
For this reason, equipment selection should consider the power supply and induction coil together.
What Is Coil-to-Workpiece Coupling?
Coupling refers to how effectively electromagnetic energy is transferred from the induction coil to the workpiece.
The distance between the coil and the component has a major influence on this transfer.
If the coupling distance becomes unnecessarily large, energy transfer may become less effective. If the coil is positioned too close, however, mechanical clearance, loading, dimensional variation and process safety may become difficult to manage.
Industrial coil design must therefore balance:
· Electromagnetic efficiency
· Workpiece tolerance
· Component loading
· Automation
· Cooling
· Production accessibility
This is especially important for automated systems where thousands of components must repeatedly enter the same heating position.
Matching Induction Heating Equipment to the Application
Different industrial processes require different combinations of frequency, power, coil design and process control.
Application | Main Heating Requirement |
Brazing | Localized and repeatable joint heating |
Surface Hardening | Controlled surface heating followed by quenching |
Forging | Deeper, more uniform billet or bar heating |
Annealing | Controlled heating of a defined area or component |
Melting | Energy transfer into metal charge and crucible system |
General Industrial Heating | Depends on material, size and heating depth |
Induction Brazing
Induction brazing requires controlled heating around a joint so that the filler material can flow without unnecessarily heating the complete component.
The combination of frequency, power and coil geometry should match the joint size, parent materials and required cycle time.
Induction Hardening
Hardening often requires precise control of both heating depth and heating time. The heated surface is then quenched to obtain the required hardened layer.
This makes frequency selection particularly important.
Induction Forging
Forging applications usually involve larger bars or billets and require more heat penetration through the material.
Hitfar provides medium-frequency induction heating generators as well as complete induction forging furnace systems for this type of industrial heating requirement.
Induction Annealing
Annealing requirements vary significantly depending on material, component geometry and the metallurgical objective.
The process may involve localized heating or a larger heated zone, making coil design and process control important considerations.
High Frequency or Medium Frequency: Which Should You Choose?
There is no single frequency that is best for every application.
A useful starting point is:
Consider Higher Frequency When:
· The component is relatively small
· Heating needs to be localized
· The required heating depth is shallow
· A narrow surface zone must be heated
· The process involves precision brazing or localized hardening
Explore: High Frequency Induction Heaters
Consider Lower or Medium Frequency When:
· The workpiece has a larger cross-section
· Deeper heat penetration is required
· A billet or bar needs more uniform heating
· The process involves forging or other through-heating operations
Explore: Medium Frequency Induction Heaters
Consider Ultra-High Frequency When:
· Components are very small
· The heating zone must be highly concentrated
· Precision surface heating is required
· Small brazing or fine heat-treatment applications are involved
Explore: Ultra-High Frequency Induction Heaters
Final selection should still be based on testing or engineering evaluation of the actual workpiece.
Information to Provide When Selecting an Induction Heating Machine
To help an induction heating equipment manufacturer evaluate the application accurately, prepare the following information before requesting a quotation:
1. Workpiece Material
Specify the material and grade where possible.
Example:
· Carbon steel
· 304 stainless steel
· Copper
· Aluminum
· Carbide
2. Workpiece Dimensions
Provide:
· Diameter
· Length
· Wall thickness
· Weight
· Drawing or photo
3. Heating Area
Define whether you need:
· Full-part heating
· Surface heating
· End heating
· Joint heating
· Continuous strip heating
· Scanning heating
4. Starting and Target Temperature
For example:
20°C → 850°C
or
Room temperature → brazing temperature
5. Required Heating Time
Specify how quickly one part must reach the target condition.
6. Production Capacity
Provide pieces per hour, kilograms per hour or required cycle time.
7. Process After Heating
Explain whether the component will undergo:
· Brazing
· Quenching
· Forging
· Annealing
· Press fitting
· Melting
· Forming
These details are far more useful than requesting an "induction heater for steel" without process information.
Common Induction Heating Equipment Selection Mistakes
Selecting Only by Kilowatt Rating
Higher power does not automatically mean a better process. An incorrectly selected frequency or coil can still create poor heating distribution.
Selecting the Highest Frequency Available
Higher frequency usually produces more concentrated surface heating. It is not automatically suitable for large components requiring deep heat penetration.
Ignoring Coil Design
A standard coil cannot provide optimal results for every workpiece geometry.
Ignoring Production Cycle
Laboratory heating of one component and continuous industrial production are different operating conditions.
Providing Incomplete Material Information
Material properties directly affect heating behavior. Exact material grades improve equipment selection accuracy.
Ignoring Automation Requirements
For mass production, equipment selection should consider loading, positioning, heating, quenching, unloading and PLC/CNC integration from the beginning.
Why Industrial Manufacturers Use Induction Heating
When correctly engineered for the workpiece, induction heating can provide several manufacturing advantages:
· Fast heat-up
· Localized heating
· Repeatable heating cycles
· No direct flame
· Good process controllability
· Easier integration with automated production
· Reduced unnecessary heating of surrounding areas
· Precise heating of selected component zones
The actual efficiency and production benefit depend on the application, equipment configuration and process design.
For this reason, induction heating should be treated as an engineered manufacturing process, rather than simply as an alternative type of heater.
Choosing an Induction Heating System with Hitfar
Hitfar develops induction heating equipment covering medium-frequency, high-frequency and ultra-high-frequency heating for industrial processes including brazing, hardening, annealing, forging and metal heating.
Instead of selecting equipment only according to machine power, the heating system should be matched to the actual workpiece and production target.
When evaluating your application, prepare:
Material + dimensions + heating area + target temperature + heating time + production rate
These parameters help determine the appropriate:
· Frequency range
· Power level
· Induction coil
· Cooling configuration
· Heating method
· Automation requirements
Frequently Asked Questions About Industrial Induction Heating
What frequency is best for induction heating?
There is no single best frequency. Higher frequencies generally favor more concentrated surface heating, while lower frequencies allow deeper electromagnetic penetration. The correct frequency depends on material, workpiece dimensions, heating depth and process requirements.
Is high-frequency induction heating better than medium-frequency heating?
Not necessarily. High-frequency induction heating may be better for smaller parts and localized heating, while medium-frequency heating is often more suitable for larger cross-sections and deeper heating. Equipment should be selected according to the application rather than frequency alone.
How much power does an induction heater need?
Required power depends on the workpiece mass, material, temperature rise, heating time, coil efficiency and production rate. Providing the workpiece dimensions and required heating cycle allows the manufacturer to evaluate the appropriate power range.
Can induction heating heat stainless steel?
Yes. Stainless steel can be heated by induction, but different stainless-steel grades have different magnetic, electrical and thermal properties. Equipment settings and coil design therefore need to match the actual alloy and workpiece.
Can induction heating heat copper and aluminum?
Yes. Copper and aluminum can be heated by induction, although their high electrical and thermal conductivity can require different equipment and process parameters compared with steel.
What is the difference between induction heating and flame heating?
Flame heating transfers heat from a combustion source to the surface of the workpiece. Induction heating generates heat directly in the conductive workpiece through electromagnetic induction. This makes it possible to heat selected areas without direct flame contact.
Why is the induction coil important?
The induction coil controls where electromagnetic energy is concentrated around the workpiece. Its shape, size, number of turns and distance from the component affect heating distribution, coupling efficiency and repeatability.